Precision machiningVOLM's critical production equipment is supplied by world-leading brands.Learn more
Quality controlGuided by domestic and international standards, VOLM applies an integrated quality management system across the complete production process.Learn more
Quality controlGuided by domestic and international standards, VOLM applies an integrated quality management system across the complete production process.Learn more
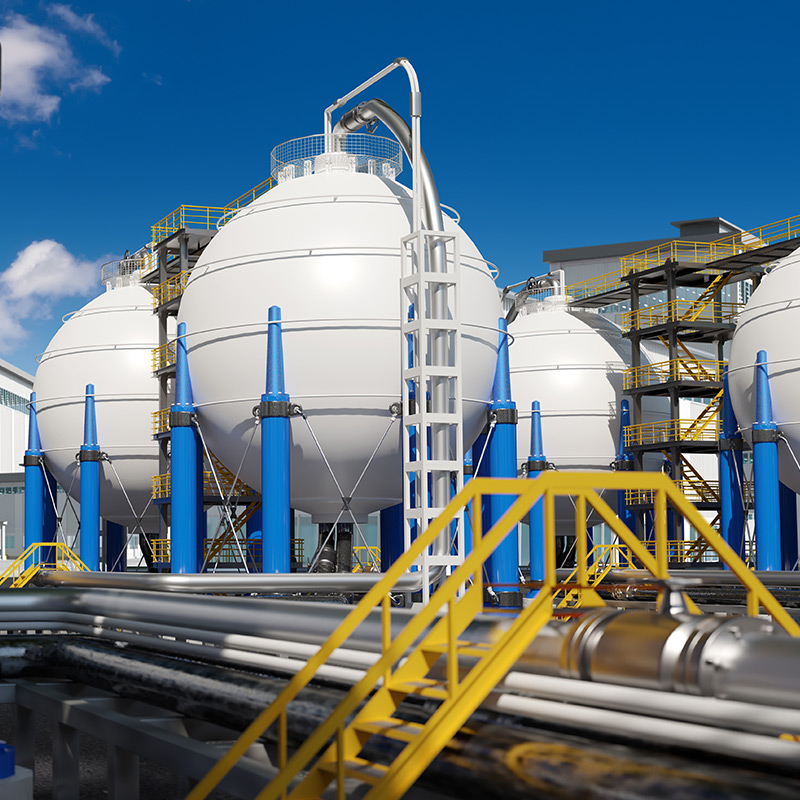
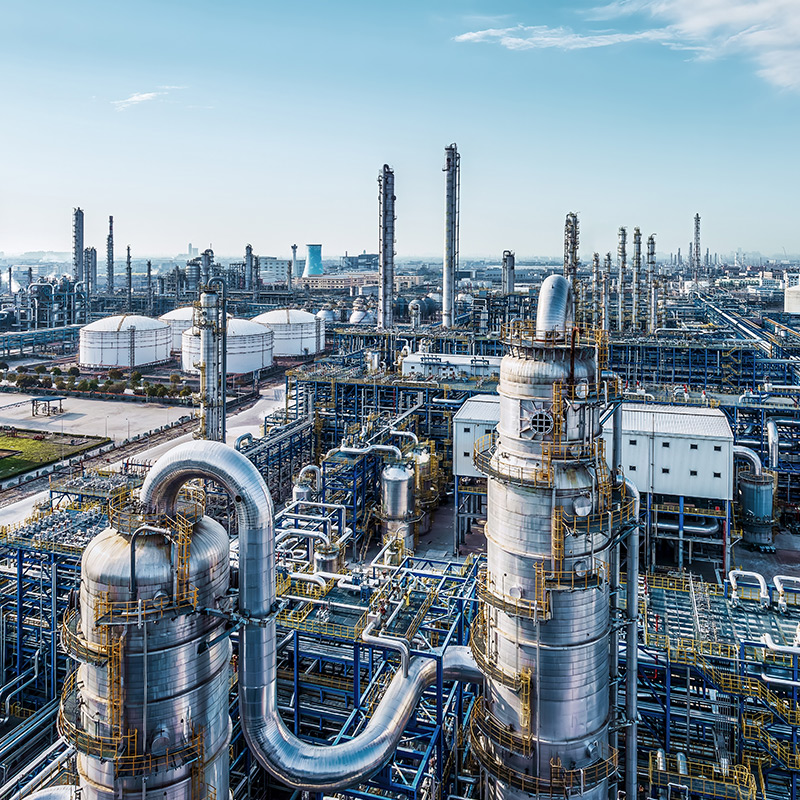
Petrochemical and coal chemicalPSA, residue hydrogenation, chlorine compression, VCM recovery and ethylene compression.Learn more
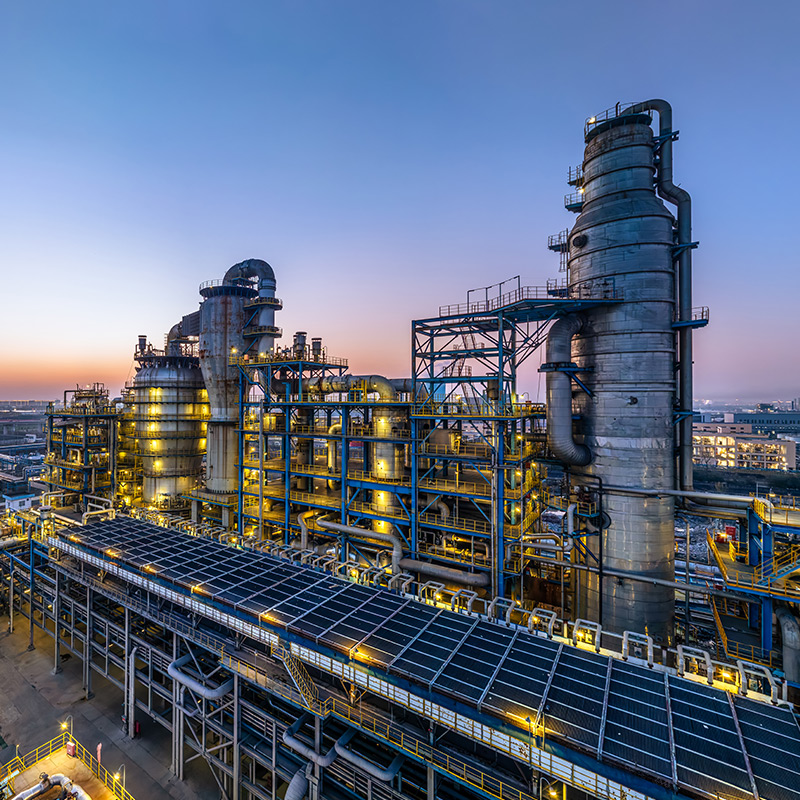
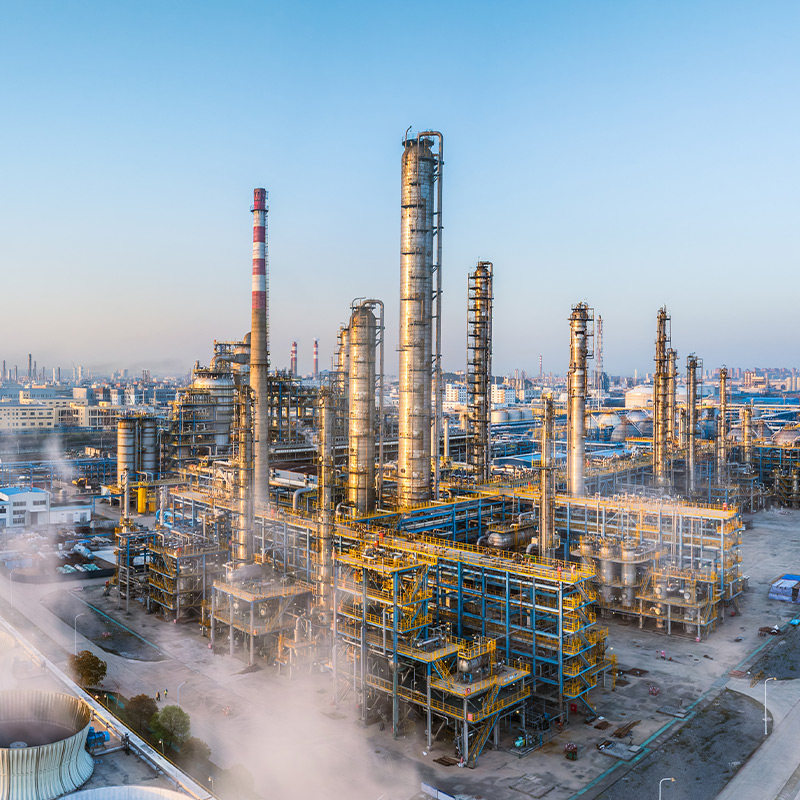
RefiningCrude distillation, hydrodesulfurization, hydrocracking, FCC and catalytic reforming.Learn more
Volm Screw Vacuum Systems Successfully Replace Top-Tier International BrandsMore than 50 Volm systems were ordered after operating performance improved dramatically.Learn more
Volm VMB05 Double-Casing Multistage Centrifugal Pump in 200 kt/a Alkane-Aromatic UnitAn engineered replacement for hazardous hydrogenation feed service at 8.5 MPa.Learn more
Professor Ba Dechun of Northeastern University interviewed by VOLMVOLM vacuum pumps are recognized for precision, high standards and innovation.Learn more
VOLM Petrochemical Pump Research Center establishedA joint research center with the national pump product quality inspection center.Learn more
Volm Screw Vacuum Systems Successfully Replace Top-Tier International Brands Volm Screw Vacuum Systems Successfully Replace Top-Tier International Brands In 2019, a leading chemical enterprise in China faced critical equipment failures in its core production line. Since its commissioning in 2017, their internationally branded screw vacuum systems had suffered progressive performance degradation, directly impacting production stability. Mr. Li, Head of Equipment Department, stated: "The system’s designed capacity was 200 tons/hour, but actual output dropped to 150 tons/hour with escalating maintenance costs." After installing Volm’s screw vacuum systems in August 2019, operational data showed dramatic improvements. Over subsequent years, the company ordered 50 vacuum systems from Volm, fully replacing the original international brand. View details
Race Against Time: Volm Vacuum Pumps Secure Production in 32°C Heatwave Race Against Time: Volm Vacuum Pumps Secure Production in 32°C Heatwave In the summer of 2022, a fine chemical plant in East China faced critical production bottlenecks in solvent recovery. Their existing liquid ring-Roots system suffered vacuum degradation from the designed -0.098 MPa (G) to -0.07~-0.08 MPa (G) at ambient temperatures ≥32°C. This caused downstream Roots pumps to fail, forcing production cuts. Plant Manager Wang noted: "Last July-August, weekly output averaged just 6 tons with moisture content spiking to 12%, driving customer complaints up 400% YoY." To address energy efficiency and yield demands, Volm replaced the system with a screw-Roots system (DMY600 Roots + DMY300 Roots + ESDP900 Screw Pump), enabling year-round stable operation. View details
Volm Two-Stage Vacuum Compressors Revolutionize SINOPEC Waste Gas Processing Volm Two-Stage Vacuum Compressors Revolutionize SINOPEC Waste Gas Processing Driven by China’s "Dual Carbon" policy, chemical plants face stricter emission standards, with legacy systems plagued by high failure rates, inefficiency, and excessive footprint. For a SINOPEC chemical plant, Volm Pump engineered an integrated two-stage vacuum compressor solution, replacing traditional "vacuum pump + compressor" systems to achieve 60% lower failure rates and 20% higher efficiency, delivering a compact, high-safety solution for hazardous waste gas treatment. View details
Volm Conical Liquid Ring Compressors: Safeguarding Green Chemical Production—AMPS/AMPS-Na Case Study Volm Conical Liquid Ring Compressors: Safeguarding Green Chemical Production—AMPS/AMPS-Na Case Study Under global green chemistry trends, AMPS and AMPS-Na have replaced traditional toxic additives. In one production project, compressing 1,000 Nm³/h acrylonitrile-containing gas to 0.55 MPa(G) demanded extreme safety—acrylonitrile ignites upon heat exposure, releasing toxic fumes. Volm’s HPM Conical Liquid Ring Compressor, using acrylonitrile as working fluid, delivered a breakthrough solution. View details
Volm Two-Stage Liquid Ring Vacuum Pumps Empower Efficient and Stable PVC Production Volm Two-Stage Liquid Ring Vacuum Pumps Empower Efficient and Stable PVC Production In PVC suspension polymerization processes, vacuum pumps are critical across six core stages: reactor deoxygenation, post-polymerization degassing, wet material drying, and monomer recovery. Particularly in vacuum drying, maintaining 60~80°C is essential to protect PVC’s heat-sensitive particles from thermal degradation. The client requires 5~15 kPa(A) vacuum (far below single-stage liquid ring pump’s efficient range of 20 kPa(A) to atmospheric pressure). Leveraging deep industry expertise, Volm Pump delivered a customized two-stage liquid ring vacuum pump solution, ensuring stable performance across all PVC production stages. View details
Volm Vacuum Pumps Solve Blackwater Treatment Challenges at Coal Deep-Processing Base Volm Vacuum Pumps Solve Blackwater Treatment Challenges at Coal Deep-Processing Base A leading Chinese coal deep-processing facility faced multi-faceted challenges in gasification blackwater treatment, including corrosive media, temperature sensitivity, high-altitude operation (1,100m), and complex vibration conditions. Leveraging 20+ years of industrial vacuum expertise, Volm delivered a customized solution ensuring reliable long-term performance under extreme conditions. View details
Volm Liquid Ring Compressors Enable Efficient Desulfurization & Green Emission Reduction in Sichuan High-Sulfur Gas Field Volm Liquid Ring Compressors Enable Efficient Desulfurization & Green Emission Reduction in Sichuan High-Sulfur Gas Field A high-sulfur gas field in Sichuan faced plummeting desulfurization efficiency (40%) in its gas stripping system due to water quality changes, resulting in effluent sulfur levels of 1,500 mg/L. This triggered excessive chemical consumption, sludge buildup, and environmental violations. Volm Pump’s customized vacuum stripping solution delivered 90% desulfurization efficiency and 150 mg/L effluent sulfur, cutting chemical costs by 74% while eliminating H₂S leakage risks. View details